Find ATEX, IECEx, Explosion Protection & Hazardous Area Content...

News

Evidence Before Engineering Certainty

By Martin James

For forty years I’ve worked around electrical, instrumentation and control systems, including hazardous areas, ATEX, process environments and industrial automation. One thing has become increasingly obvious to me: the difficult part of using AI in engineering isn't getting an answer. It's knowing whether the evidence actually supports the answer.

AI is becoming remarkably good at finding patterns, generating explanations and producing apparently convincing technical conclusions. But engineering decisions don't happen in a text box. They happen around real assets, real measurements, real operating conditions and real consequences.

That creates a problem. An AI system can look at a dataset and say that a pump is failing. But what does the evidence actually establish? Is the asset correctly identified? Is the measurement relevant? Do we have a trustworthy baseline? Was the equipment operating under comparable conditions? Could there be another explanation? Is the data complete? Has anything been changed since the evidence was collected?

And perhaps most importantly: does the evidence prove the claim, or merely make the claim plausible? These are not the same thing.

Measurement is not proof

I've spent much of my working life dealing with systems where the difference between an indication and a conclusion matters. A transmitter can indicate a condition. A trend can reveal a pattern. An alarm can tell us that something has crossed a threshold. None of those things, by themselves, necessarily establish causation.

Yet when AI is introduced, there is a temptation to move rapidly from data → pattern → explanation → decision. I believe we need another discipline in between: evidence → challenge → contradiction → provenance → decision.

That is one of the ideas behind a system I have been developing called AVAKIMEXA.

AVAKIMEXA

AVAKIMEXA is being developed around a simple proposition: AI can generate a claim. The evidence must decide whether that claim survives.

The system is deliberately positioned at the boundary between machine intelligence and consequential engineering decisions. It does not replace the engineer. It does not take control of the plant. It does not write to PLCs, SCADA, SIS, DCS or actuators. The human remains the authority.

The purpose is different. AVAKIMEXA asks whether the evidence available is sufficient to support the claim being made. Sometimes the answer may be SUPPORTED. Sometimes CONTRADICTED. Sometimes UNRESOLVED. And sometimes the correct engineering answer is simply: INSUFFICIENT EVIDENCE. STOP.

That last answer is important. In engineering, refusing to manufacture certainty can be more valuable than producing another confident prediction.

The evidence obligation belongs to the claim

One principle has become central to my thinking: the evidence required to pass is determined by the claim — not by how convincing the existing evidence appears.

If someone claims that a pump is failing because of bearing degradation, for example, the question isn't whether the available trend looks like bearing degradation. The question is what evidence is actually required to establish that claim.

Asset identity, relevant measurements, operating conditions, baseline behaviour, time relationship, alternative explanations, data provenance, and whatever other evidence is material to that particular claim.

If a material obligation is missing, the system should not quietly fill the gap with confidence. It should expose the gap. That changes the conversation from “What does the AI think?” to “What can we actually prove?”

This matters particularly in safety-critical environments

In hazardous-area and process environments, evidence quality is not an academic issue. An incorrect assumption can influence maintenance, inspection, operational decisions and ultimately safety. The same applies as AI moves further into industrial environments.

We are likely to see increasingly sophisticated systems recommending actions based on increasingly large quantities of data. More data does not automatically mean more proof, and a more sophisticated model does not automatically make incomplete evidence complete.

That is why I think the next stage of industrial AI needs to be less about making machines sound certain and more about making uncertainty visible.

Human authority still matters

There is another boundary I consider non-negotiable. AI should assist engineering judgement. It should not quietly become engineering authority.

The engineer needs to be able to see what evidence was considered; what evidence was missing; what contradictions were found; where provenance matters; what assumptions were made; and why the system stopped or allowed a claim to proceed.

That creates something different from another predictive AI platform. It creates an evidence-adjudication layer between machine intelligence and consequential decisions.

The question I think industry should be asking

We have spent enormous effort asking whether AI can predict, classify, detect and recommend. I think we now need to ask another question: can the AI prove that the evidence it relied upon actually supports the claim it is making?

Because there is a fundamental difference between finding a pattern and proving what caused it. And there is an even bigger difference between generating a recommendation and having sufficient evidence to act on it.

My work on AVAKIMEXA is an attempt to explore that boundary. I am not claiming that AI should replace engineers. Quite the opposite. I am building around the idea that as machine intelligence becomes more capable, human authority becomes more important, not less.

The future industrial AI system may not be the one that gives the fastest answer. It may be the one that knows when the evidence says: Stop. We don't know yet.

Evidence. Not Guesswork.


Hazardous-area maintenance and emergency readiness aboard commercial vessels

Electrical and mechanical equipment aboard commercial vessels can operate in environments where flammable gases or vapours create a risk of fire or explosion. Tankers and vessels carrying certain hazardous cargoes require particularly careful control of equipment installed in classified areas. Shipboard engineers must understand how maintenance activities affect explosion protection while remaining prepared to respond to emergencies at sea. These responsibilities require both technical competence and an understanding of the vessel's safety procedures, particularly when equipment faults arise during a voyage.

Connect hazardous-area maintenance with maritime safety

Equipment maintenance in a hazardous area requires engineers to understand the conditions that could create an ignition source. Electrical inspections may involve checking enclosure integrity, cable entries, earthing arrangements and the condition of components used to maintain an equipment protection concept.

The International Convention on Standards of Training, Certification and Watchkeeping for Seafarers (STCW) establishes minimum international training and competence requirements for seafarers. Relevant STCW courses  develop maritime safety and emergency-response skills that support engineers carrying out their duties aboard commercial vessels.

The convention is maintained by the International Maritime Organization , which establishes an international framework for seafarer competence. Engineers working on vessels with hazardous areas may require additional specialist qualifications appropriate to their technical duties, including training relevant to explosion-protected equipment.

This combination allows personnel to approach maintenance with an understanding of the equipment and the shipboard environment in which the work takes place.

Preserve explosion protection during maintenance

Explosion-protected equipment is designed to prevent ignition under specified operating conditions. Its protective properties can be compromised if maintenance changes the equipment's construction or allows environmental damage to affect critical components.

Engineers should inspect equipment according to the manufacturer's instructions and the applicable explosion-protection standards. Particular attention may be required where vibration, corrosion or repeated maintenance has affected the condition of enclosures and connections.

Replacement components must be suitable for the equipment's certification and intended use. Installing an unsuitable cable gland, modifying an enclosure or replacing a component without considering its protection concept can compromise the original design.

Maintenance records should document the condition of the equipment, work performed and any outstanding defects. This information helps the vessel's engineering team track deterioration and make informed decisions about future inspections.

Maintain control of hazardous-area work

Shipboard maintenance should be planned around the vessel's operating conditions and the potential presence of flammable atmospheres.

Work involving electrical equipment or other potential ignition sources may require specific permits, isolation arrangements and atmospheric testing. The appropriate controls depend on the vessel's hazardous-area classification, the nature of the work and its safety management procedures.

Coordination with the vessel's responsible officers is particularly important when maintenance could affect cargo operations or other activities involving flammable substances.

Prepare engineers for shipboard emergencies

An engineer working aboard a vessel may need to respond to an emergency involving equipment outside their immediate maintenance responsibilities. Fire, flooding or an incident involving hazardous cargo can require personnel to follow established emergency duties under difficult operating conditions.

An STCW basic safety training course  provides foundational preparation for these situations. The training covers personal survival techniques, fire prevention and firefighting, elementary first aid, and personal safety and social responsibilities.

These subjects are especially relevant to personnel whose normal duties involve machinery or electrical equipment. An engineer may recognise an equipment fault during routine maintenance but must also understand how to raise the alarm and respond safely if the situation develops into a wider shipboard emergency.

The training establishes a common foundation for emergency preparedness, while the vessel's safety management system defines the specific actions and responsibilities expected of individual crew members.

Connect equipment faults with emergency procedures

Hazardous-area maintenance and emergency planning should inform one another. A recurring equipment defect may indicate a deterioration mechanism that needs to be addressed before it creates a more serious problem.

Engineers should ensure that significant defects are reported through the vessel's established maintenance and safety procedures. Where an equipment failure could affect fire detection, ventilation or other protective systems, the implications for continued operation should be assessed before work proceeds.

Emergency exercises provide an opportunity to understand how technical failures could influence the crew's response. An engineer familiar with the vessel's electrical distribution and machinery arrangements can contribute useful information about equipment isolation and the restoration of essential services.

Maintain technical competence and emergency readiness together

Safe maintenance aboard vessels with hazardous areas depends on correctly maintained equipment, competent personnel and effective operational controls.

Engineers need to preserve the protective properties of equipment during maintenance while understanding their responsibilities within the vessel's emergency arrangements. Integrating technical inspections with maritime safety training and established reporting procedures helps crews identify developing hazards and respond appropriately when equipment problems affect shipboard safety.

New Encapsulation Rules: What Changes for Your Ex Design?

Encapsulation protection, or “m”, is a protection technique used to prevent ignition in equipment for explosive atmospheres across oil and gas, mining and other industrial applications.

For over 10 years, manufacturers of encapsulated equipment for explosive atmospheres have worked to IEC 60079-18:2014 and its subsequent amendment. IEC 60079-18:2025, Edition 5.0, is the first full technical revision of the encapsulation “m” standard since then.

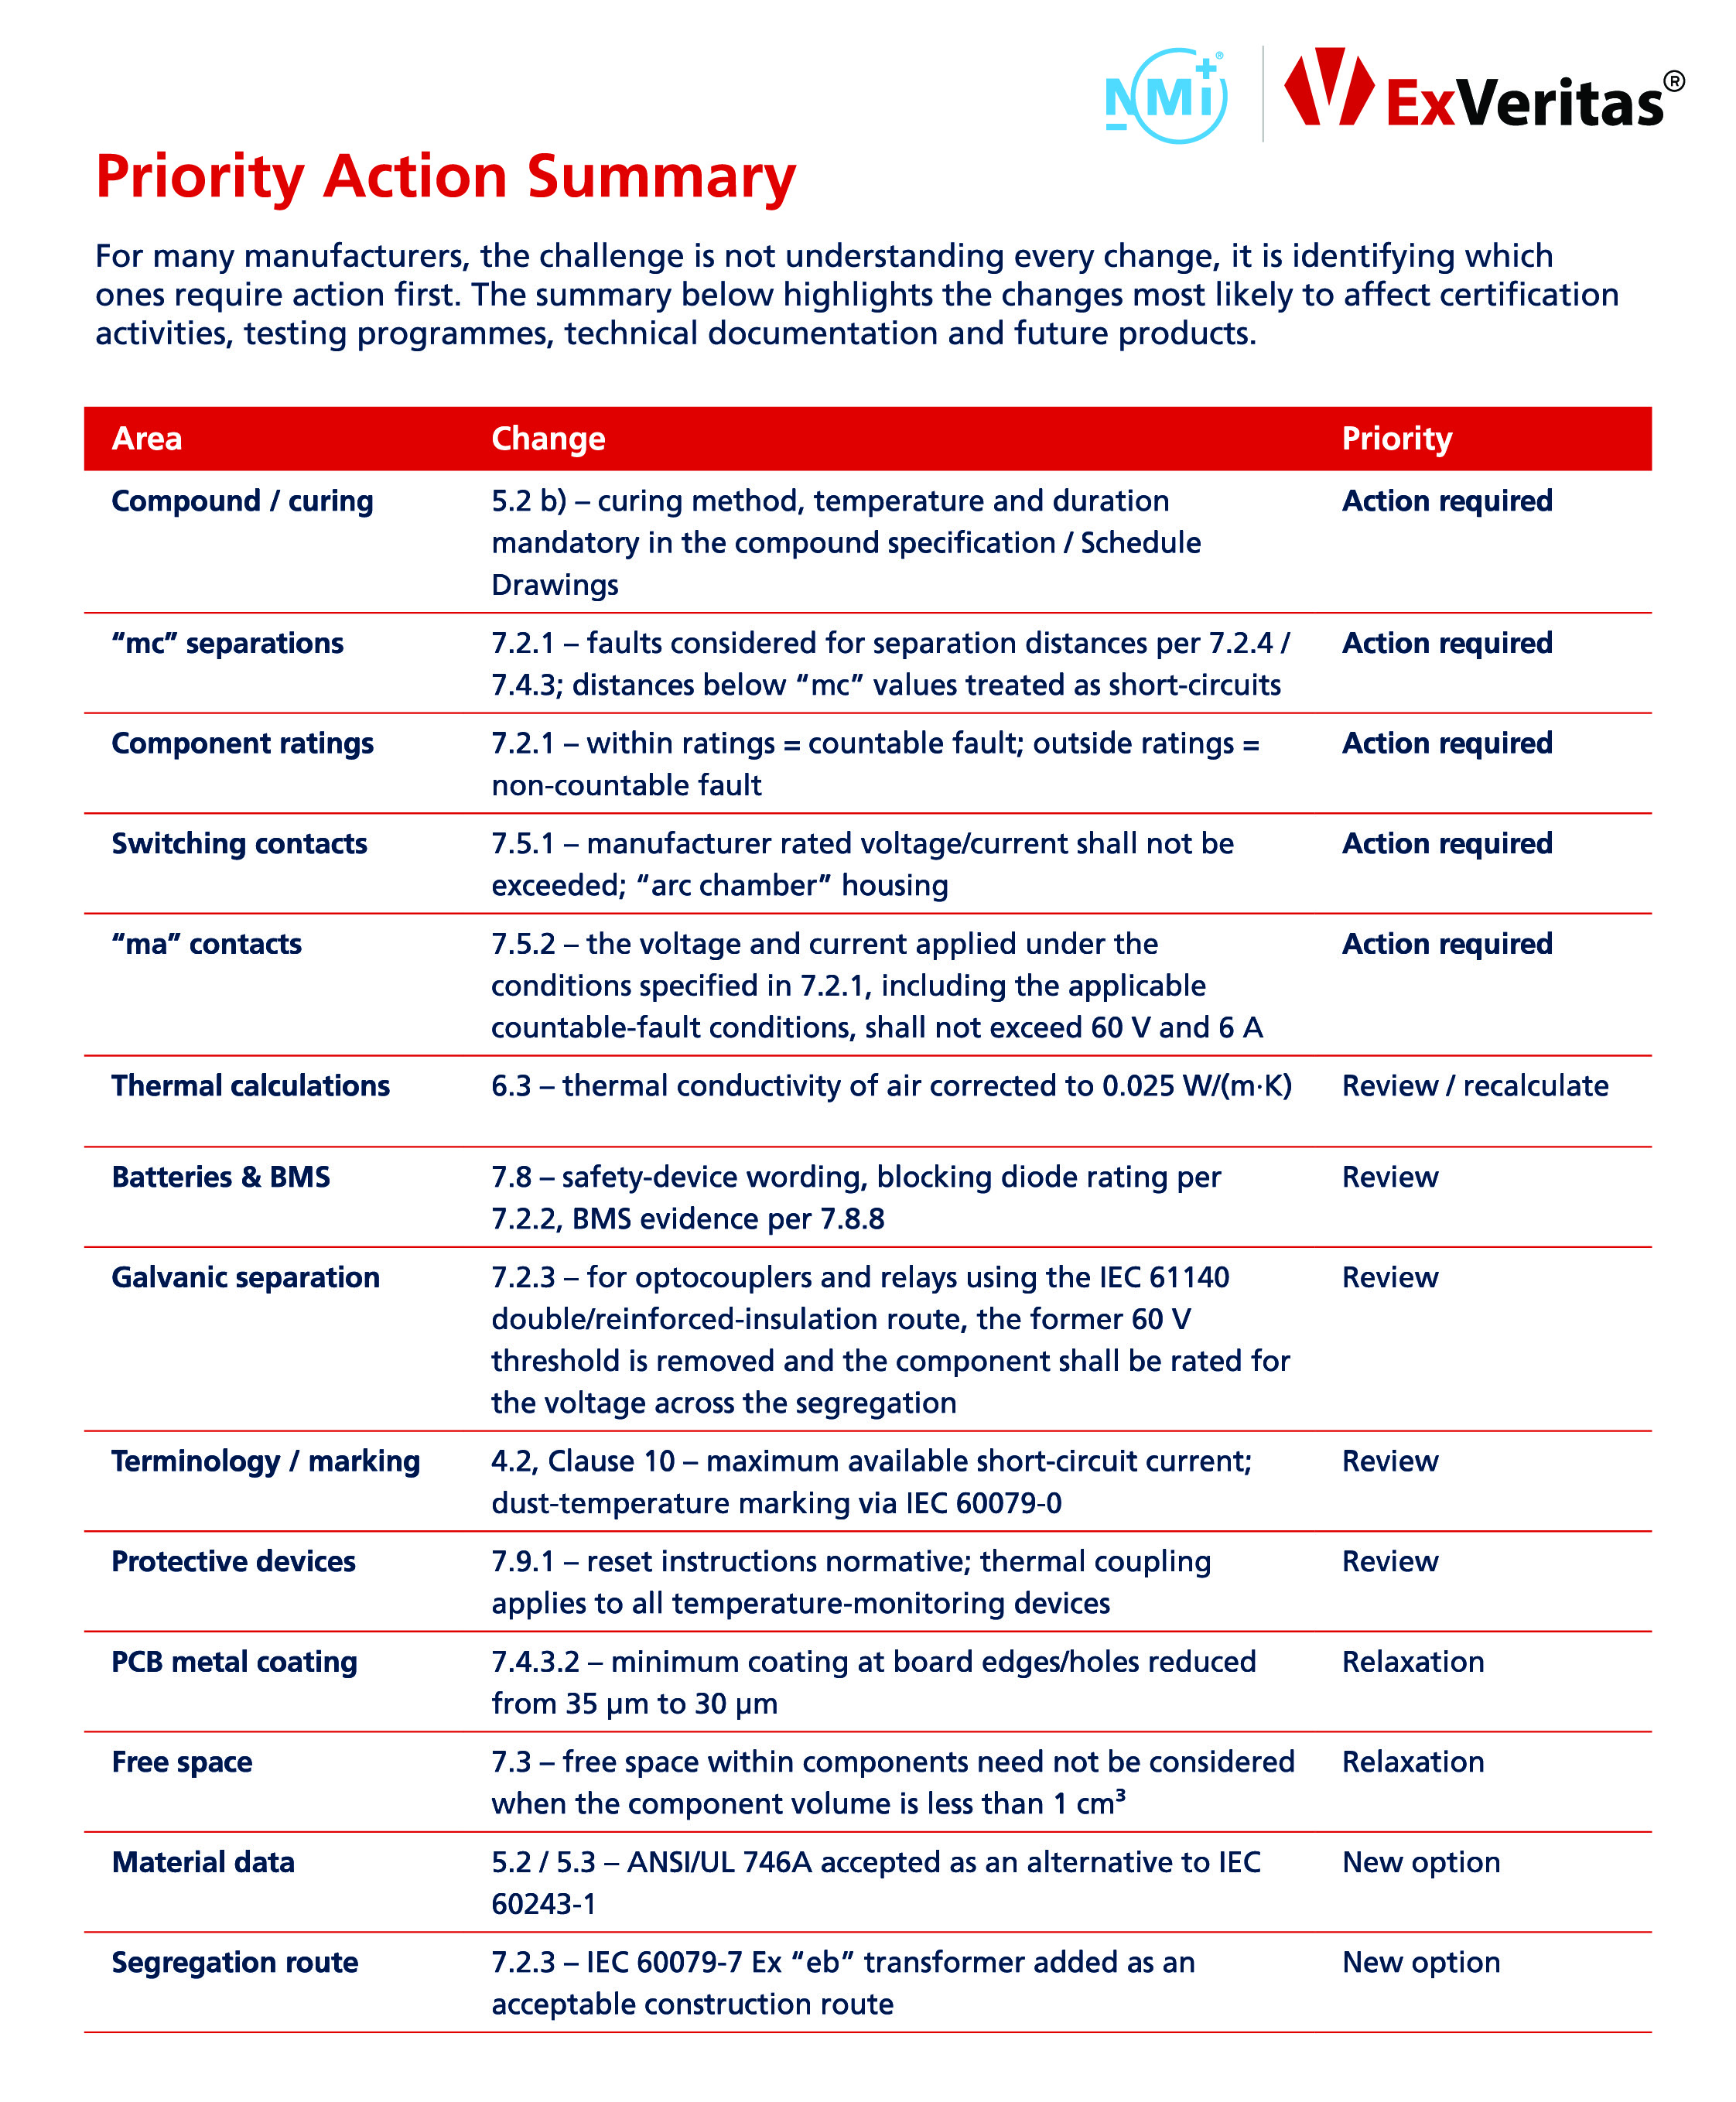
While the fundamental protection concept remains unchanged, Edition 5 introduces four Major Technical Changes. For manufacturers, the important question is not simply what has changed, but which changes could affect existing products, new designs and future certification.

Where are the significant changes?

The following areas deserve attention first because they include the Major Technical Changes and other changes with significant practical impact on the design and certification of encapsulated equipment.

Compound specification and curing

Edition 5 requires the curing method, temperature and duration to be included within the controlled compound specification.

This makes curing conditions an explicitly controlled part of the design and manufacturing process. Manufacturers should consider whether this information is already adequately captured within their controlled documentation. Where curing conditions are recorded elsewhere, documentation updates may be required.

Fault examination for “mc”

Edition 5 expressly applies the relevant separation-distance requirements to “mc”. Compact designs therefore cannot disregard these requirements simply because faults are generally not considered for “mc”.

Component fault treatment is also clarified. A component operating within its manufacturer ratings is treated as a countable fault, while operation outside those ratings is treated as a non-countable fault.

For compact “mc” equipment or designs relying on highly-stressed components, these provisions warrant particular attention.

Encapsulated switching contacts

The rated voltage and current specified by the switching-contact manufacturer must not be exceeded, while the housing around the arcing area is now termed the “arc chamber”.

For Level of Protection “ma”, the 60 V and 6 A limits must also be met under the applicable fault conditions specified by the standard. Manufacturers of “ma” equipment incorporating switching contacts should therefore verify the voltage and current under these conditions, rather than considering normal operating values alone.

Thermal calculations and battery systems

The previous edition included a note giving the thermal conductivity of air as 0.25 W/(m·K). This has been corrected to 0.025 W/(m·K).

Where the previous value was used to determine the hottest component or compound temperature, the calculation should be reviewed and, where necessary, recalculated.

Battery-powered equipment also receives additional attention.

The term “control device” is generally replaced by “safety device”, while Edition 5 introduces more explicit responsibilities where a Battery Management System provides a protection required by IEC 60079-18.

Evidence is required that the BMS remains functional under the expected relevant malfunctions. The equipment manufacturer should retain the appropriate supporting declaration from the BMS manufacturer and include information necessary to maintain the integrity of the protection within the product instructions.

Blocking diodes used to prevent reverse current are also subject to specified rating requirements.

ExVeritas September HES Content Image 2 PRINT

What should manufacturers do now?

A structured gap assessment remains the clearest way to separate substantive technical gaps from changes with little practical impact, particularly for "mc" designs, "ma" switching contacts, and battery systems affected by the BMS provisions.

NMi ExVeritas carries out these assessments for encapsulated equipment manufacturers, mapping Edition 5 requirements against existing designs and documentation ahead of transition and certification deadlines.

https://www.exveritas.com/

Intrinsically Safe Ultrasonic Sensors for Hazardous Environments

In industries such as oil and gas, chemical processing, mining, energy, food and beverage, and material handling, measurement equipment is often required to operate where flammable gases, vapors, or combustible dust may be present. In these environments, selecting the right sensor is not only about measurement performance. It is also part of the overall safety strategy.

Intrinsic safety is an explosion-protection method that limits the electrical and thermal energy available within a circuit, helping prevent the ignition of a potentially explosive atmosphere. When properly installed with an approved intrinsic safety barrier, an intrinsically safe ultrasonic sensor can provide non-contact level and distance measurement within hazardous areas.

This makes ultrasonic sensing particularly useful for applications such as monitoring flammable liquid levels in tanks, measuring material levels, detecting objects or equipment position, and monitoring distance on process equipment. Because ultrasonic sensors operate without contacting the target material, they can also reduce exposure of the sensor to corrosive, abrasive, or otherwise difficult materials.

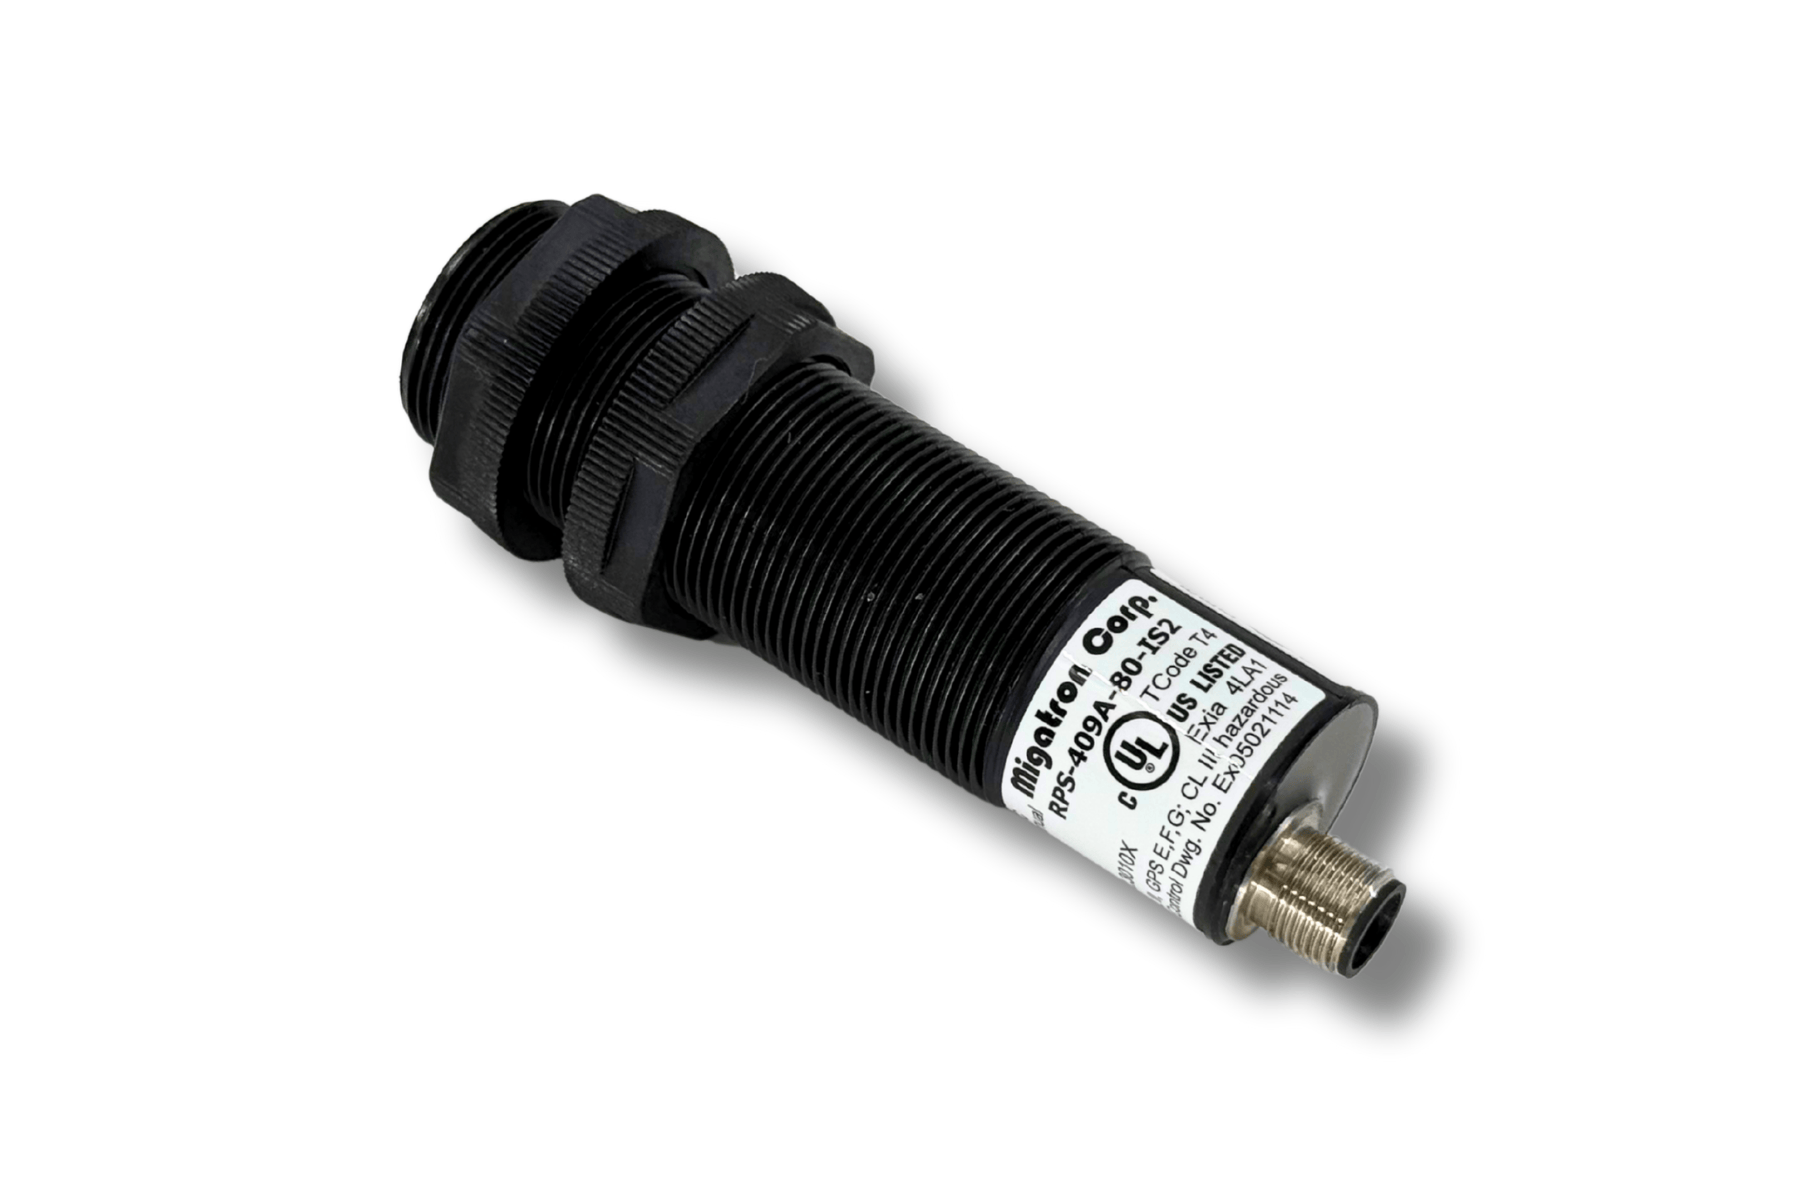
Migatron Corporation designs and manufactures intrinsically safe ultrasonic sensors for hazardous area applications. The RPS-409A-IS2 carries ANZEx, ATEX, IECEx, and C-UL-US approvals and is designed for use in mines susceptible to firedamp (Group 1 protection level Ma), and in hazardous gas and dust environments, including Zones 0, 1, 2, 20, 21, and 22 and Class I, II, and III locations when used with an approved intrinsic safety barrier(s). The RPS-429A-IS also offers ATEX, IECEx, and C-UL-US approvals, with 4–20 mA current-loop or 1–5 V analog output options.

As automation expands into hazardous environments, safe and reliable measurement becomes increasingly important. Migatron also works directly with OEMs and engineers to develop customized ultrasonic sensing solutions tailored to specific application and integration requirements.

http://www.migatron.com/

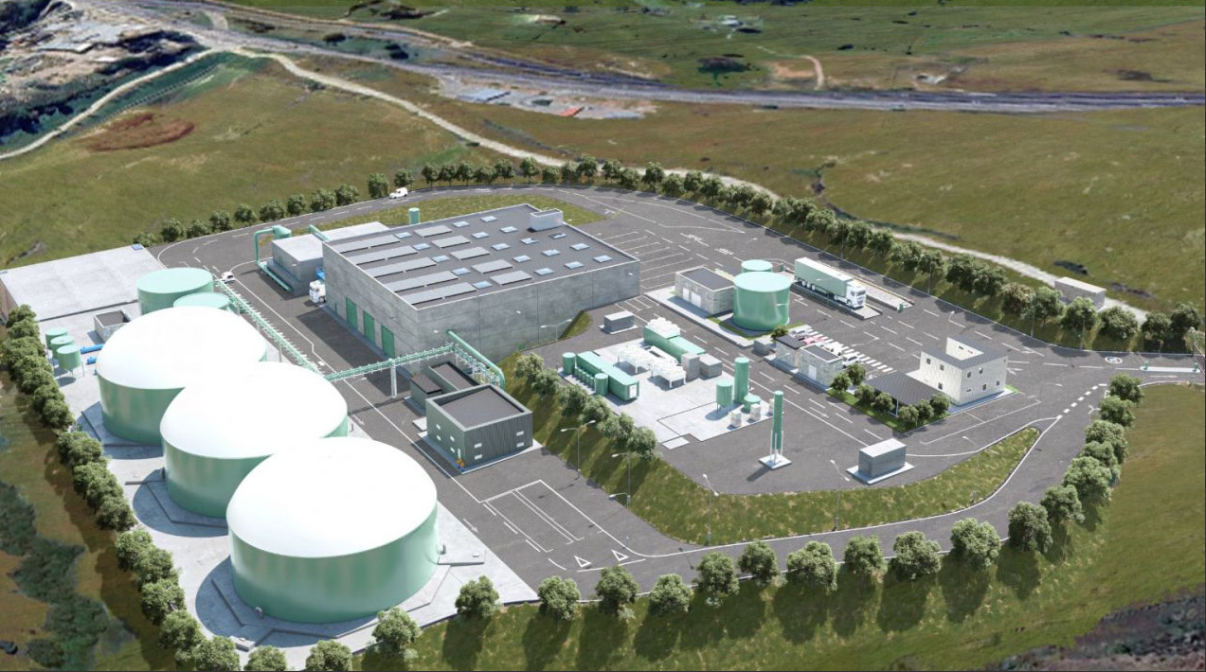
WELTEC BIOPOWER has begun construction of a new biomethane plant in Colmenar Viejo, north of Madrid, alongside environmental services provider PreZero and Enagás Renovable.

weltec_3.jpeg

Once operational, the facility will generate up to 60 GWh of renewable energy annually, enough to meet the energy requirements of approximately 11,700 households or 30,000 residents.

The plant will process up to 75,000 tonnes of organic waste each year, including separately collected household biowaste from Colmenar Viejo and surrounding municipalities. Rather than being sent to landfill, the organic material will be converted into renewable biomethane.

At the heart of the facility will be three stainless-steel digesters supplied by WELTEC BIOPOWER. Each digester measures 25.34 metres in diameter and 10.05 metres in height, with a capacity of 5,067 cubic metres. A gas-tight pre-storage tank will help maintain a continuous substrate supply and stable operating conditions.

“Stainless steel is particularly resistant to corrosion under the demanding biological and chemical conditions found in the digestion process. This gives the plant a long service life, high operational reliability and low maintenance requirements,” said Alain Priser, International Sales Manager at WELTEC BIOPOWER.

The facility will operate as a closed and sealed system, with biofilters and activated carbon systems designed to remove up to 99% of odorous substances from exhaust air. The resulting biomethane will be injected directly into the gas grid.

The project is expected to contribute to Madrid's efforts to reduce landfill use while converting regional organic waste into locally produced renewable energy.

WELTEC BIOPOWER will provide further information about the technology at stand 276A at Salon del Gas Renovable in Valladolid, 29–30 September 2026.

ABB expands hazardous-area dust monitoring with new PFM 20 Ex

ABB has expanded its industrial emissions measurement portfolio with the launch of the PFM 20 Ex, a new dust monitoring device developed for use in hazardous and harsh industrial environments.

Designed for applications where robust equipment and low-range measurement are essential, the PFM 20 Ex provides a certified dust detection range down to 7.5 mg/m³ and meets ATEX Zone 22 certification requirements.

The new device extends ABB’s dust monitoring capabilities and forms part of the company’s wider industrial emissions measurement offering, which includes continuous emissions monitoring, particulate analysis, dust and gas flow measurement and portable hydrocarbon detection.

The launch also builds on the measurement technologies added to ABB’s portfolio following its acquisition of Födisch Group in 2024. The acquisition expanded ABB’s capabilities in dust and gas flow measurement as well as portable hydrocarbon detection.

By bringing these technologies together, ABB says industrial operators can source a broader range of emissions measurement solutions from a single supplier, helping to simplify supplier coordination and provide a more consistent approach to selecting, deploying and supporting measurement equipment across industrial facilities.

“The PFM 20 Ex is an important product launch in its own right, giving customers high-sensitivity dust monitoring for hazardous environments,” said Jean-Rene Roy, Global Business Line Manager at ABB’s Measurement & Analytics division.

“This also represents a significant addition to our highly capable industrial emission measurement portfolio, enabling us to support a broader range of customer needs, from continuous gas analysis to dust, gas flow and portable measurement.”

ABB’s industrial emissions measurement portfolio includes continuous emission monitoring systems such as the ACF5000 and MCA 10 CEMS, alongside particulate analysers including the PFM 20, PFM 13 and OPM 19 ED dust analysers. The range also incorporates the FMD 09 gas flow analyser and portable Flame Ionisation Detectors (FIDs) for real-time, on-site hydrocarbon detection.

The measurement technologies are supported by remote and on-site service capabilities and flexible care agreements. ABB’s My Measurement Assistant+ (MMA+) also provides users with access to device health information, reports, documentation and AI-powered device-specific knowledge and support.

With the addition of the PFM 20 Ex, ABB is extending its ability to support industrial operators requiring dust and emissions monitoring technologies suitable for demanding and potentially hazardous operating environments.

One radio, two worlds: How the IS380.1 keeps hazardous-area teams connected

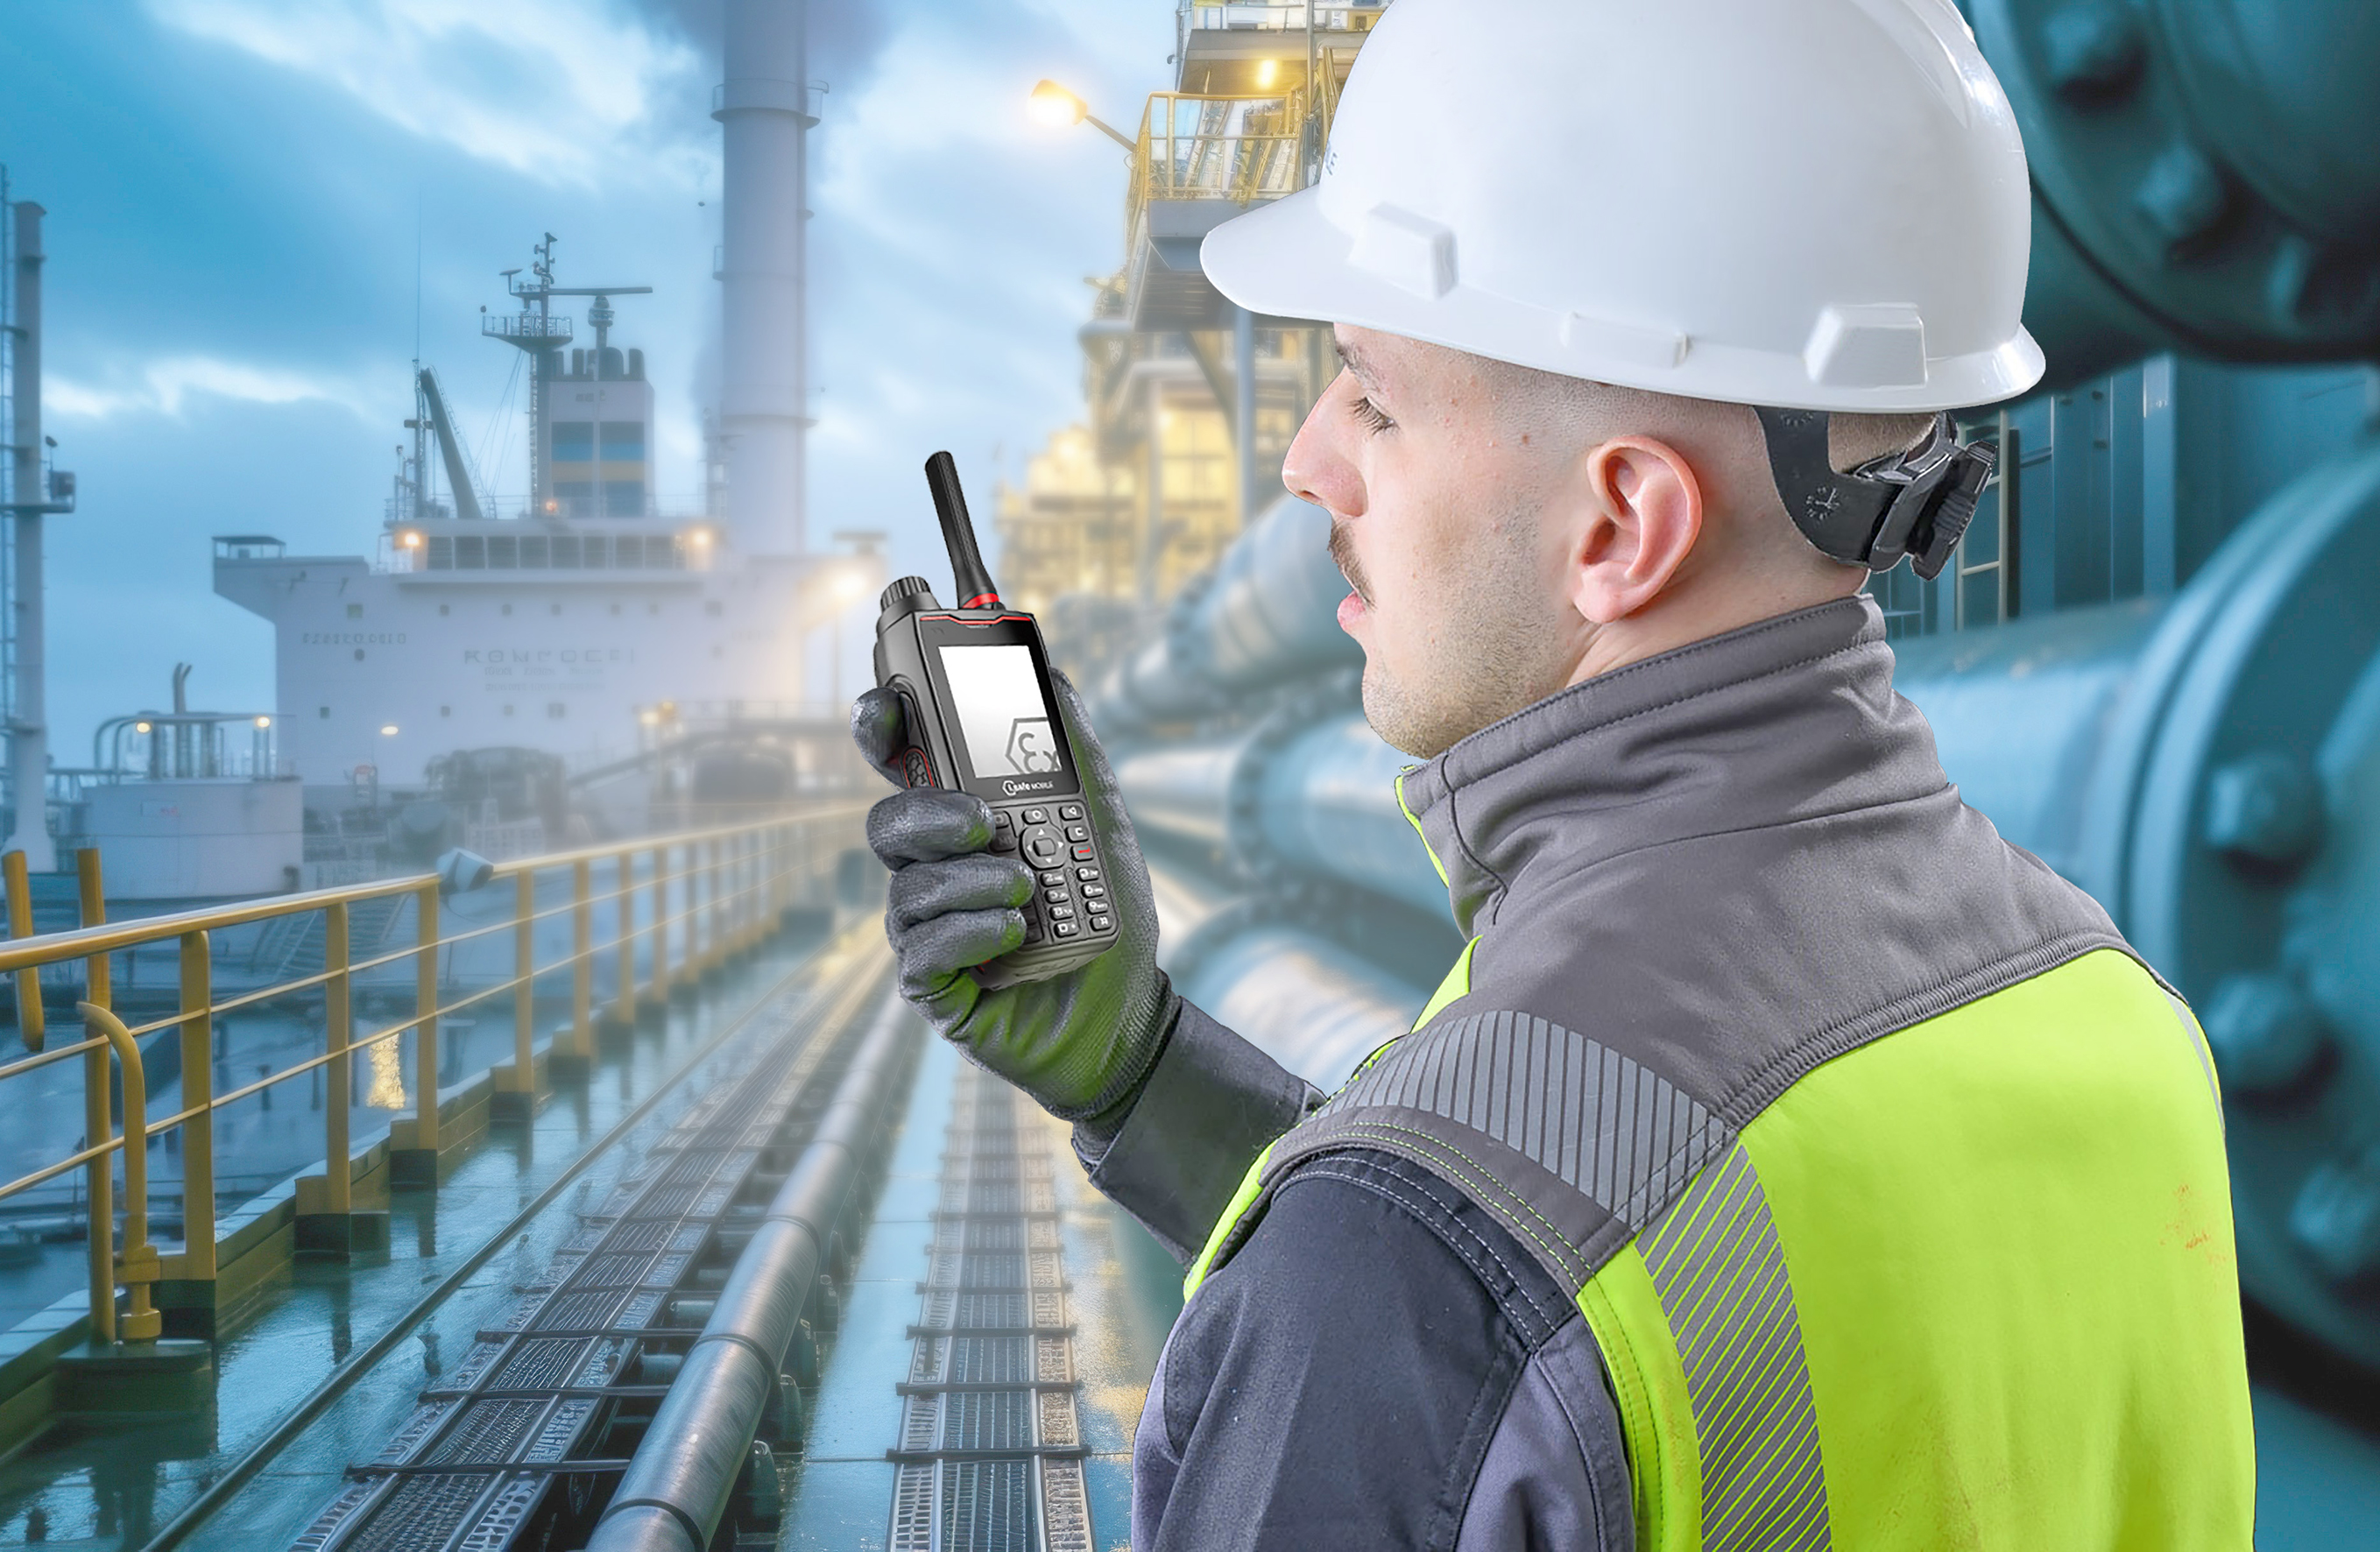
Ask any plant manager what slows down a digital rollout in a hazardous area, and the answer rarely involves the network. It involves the device in someone's hand. Field crews trust their two-way radios the way a pilot trusts a checklist: instinctively, without looking. Swap that tool for an unfamiliar smartphone and adoption stalls, however capable the new hardware might be.

i.safe MOBILE built the IS380.1 to sidestep that problem entirely. Rather than asking hazardous-area workers to relearn their tools, the company put a full 4G LTE device inside a housing that behaves like the radio they already know. Certified for ATEX and IECEx Zone 1/21, the IS380.1 targets exactly the environments where explosion protection is non-negotiable: refineries, offshore platforms, chemical plants, ports and rail infrastructure.

Ergonomics that need no explanation

Pick up the IS380.1 and every control sits where a radio operator expects it. A large, side-mounted PTT button falls naturally under the thumb. A rotary switch handles channel selection or volume without forcing eyes away from the task at hand. A front-facing, amplified loudspeaker cuts through compressor noise or a busy loading bay, and an SOS button next to the antenna offers a direct route to emergency alerting. Existing headsets and remote speaker microphones connect through the familiar 13-pin ISM interface, so accessory budgets and training materials stay valid.

For safety officers, that continuity carries real weight. Every additional training session is a session where attention drifts from the actual hazard. A device that inherits established muscle memory removes a whole category of rollout risk before it starts.

Where PMR meets broadband PTT

Underneath that familiar shell runs a powerful processor with 8 GB of RAM, 128 GB of storage, and i.safe MOBILE's own ISM-OS 16, based on Android. Connected to a 4G network, the IS380.1 opens up Push-to-Talk over Cellular alongside standard telephony, giving teams nationwide or even global reach that conventional VHF/UHF simply cannot offer.

Crucially, this does not mean abandoning existing radio infrastructure. Through third-party RoIP gateways, the IS380.1 bridges cellular PTT platforms with legacy VHF/UHF networks, so a technician carrying the new device can still reach a colleague on an older handset. Sites can migrate site by site, shift by shift, without a forklift replacement of every radio in circulation, and without a gap in coverage during the transition.

Built for the environments where it works

An IP68 rating and MIL-STD 810H certification confirm what the housing already suggests: this is hardware designed for offshore platforms, petrochemical plants and outdoor industrial sites, not for a controlled office environment. The pre-installed i.safe MOBILE App World, hosted on German servers and updated alongside device firmware, adds a further layer of control. IT and safety teams get a curated channel for validated applications, including lone-worker protection and PTT clients, tested specifically on i.safe MOBILE hardware rather than assumed to work.

A practical first step

For operators in oil and gas, chemicals, ports, rail and heavy industry, the IS380.1 offers something rarer than raw specifications: a migration path that respects how field teams actually work. It extends coverage, adds broadband PTT and telephony, and keeps legacy radio users in the conversation, all inside a form factor nobody needs to be retrained on. That combination turns digital transformation from a disruptive event into a gradual, low-risk transition, exactly the kind hazardous-area operations need.

Picture credits: i.safe MOBILE

www.isafe-mobile.com

ATEX-Rated Containerised Steam System

Engineered for hazardous environments. Designed for flexibility.

Customers across more than 80 industries rely on tailored steam solutions to meet their individual operational requirements. Where steam generation is required within potentially explosive or hazardous areas, specialist engineering is essential.

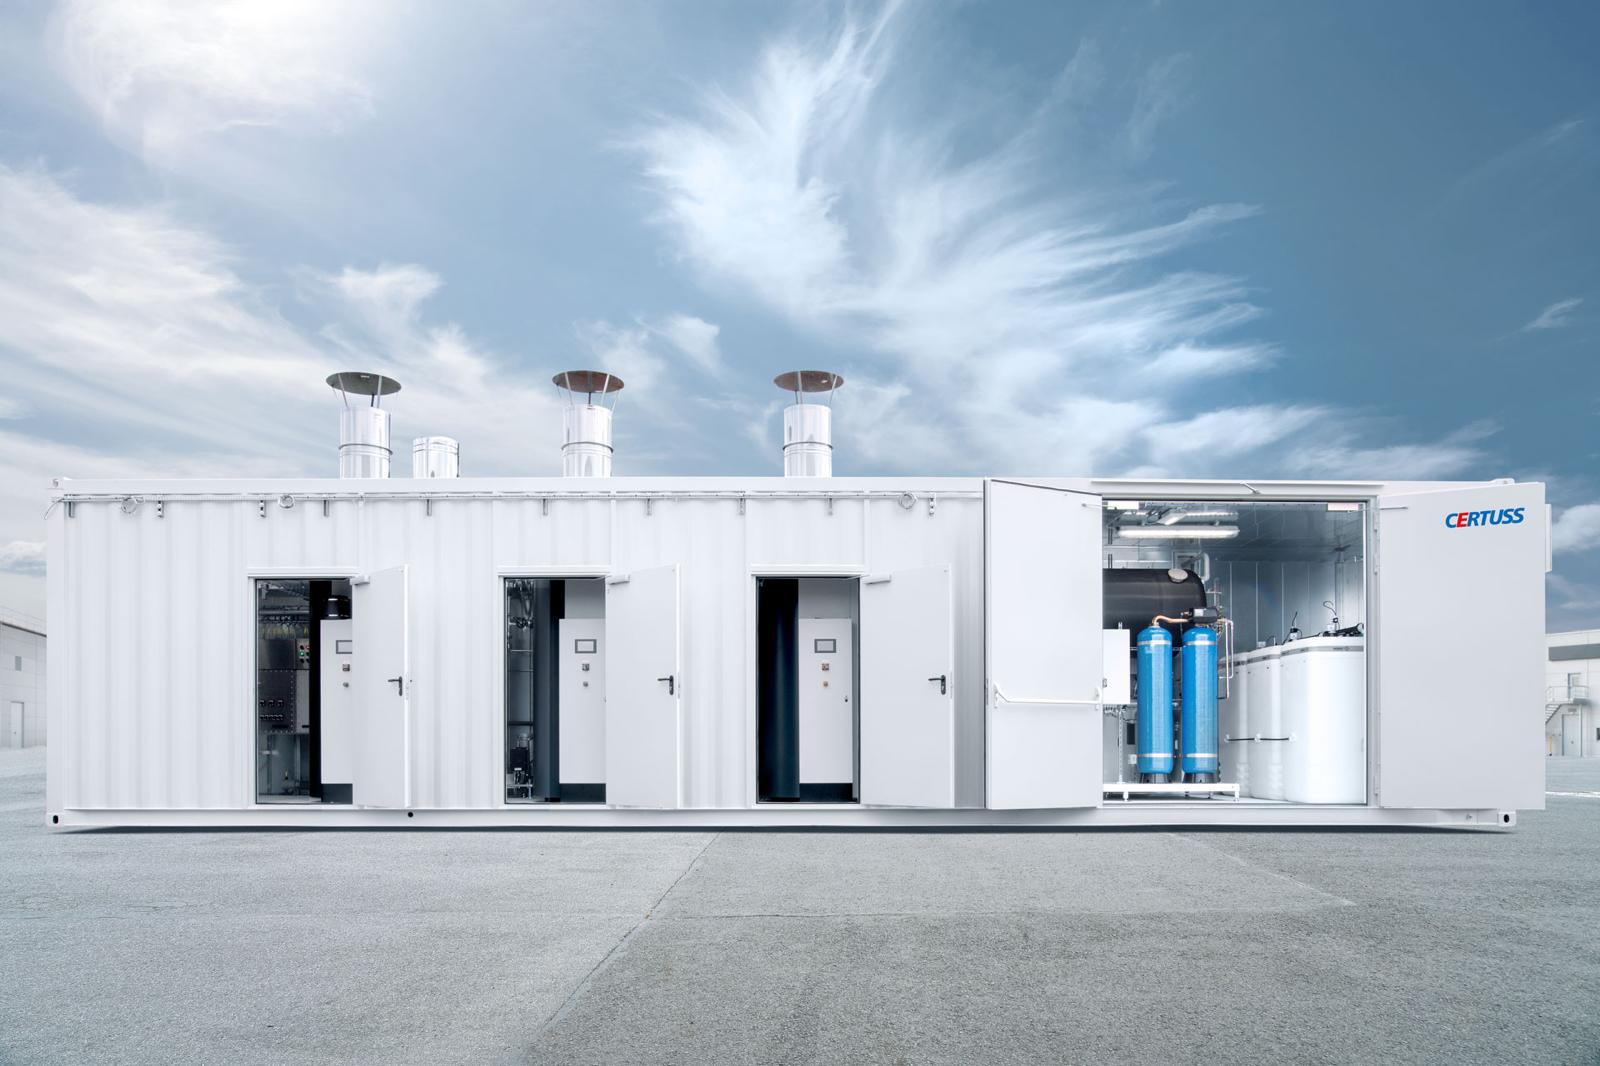
Our ATEX-rated containerised steam system has been specifically designed and engineered for use within potentially explosive environments, including refinery applications. The system combines safe, reliable steam generation with a flexible, space-saving design.

Designed for Hazardous Areas

The container has been purpose-built for operation within a potentially explosive environment. The ventilation system has been specially developed and manufactured for the application, while the control system has been custom-designed to meet the requirements of the designated hazardous zones.

By integrating these systems into a single package, the customer receives a complete solution designed around the specific requirements of the installation.

Simple, Automated Operation

A high level of automation makes the system simple and efficient to operate, reducing the need for manual intervention and helping to minimise personnel requirements.

The integrated controls provide greater flexibility and allow the system to respond to changing steam demand, giving customers a highly responsive and straightforward steam-generation solution.

Flexible and Space-Saving

Steam systems are inherently compact, but where space is particularly restricted, a containerised solution provides additional flexibility in terms of location and installation.

Housing the complete steam plant within a purpose-designed container allows the system to be positioned where it is most practical for the customer, making it particularly suitable for existing industrial facilities where space is limited or disruption needs to be minimised.

Rapid Steam Generation

The rapid steam generation technology can be ready to produce steam in approximately 3–5 minutes, allowing the system to respond quickly when steam is required.

The generator supplies only as much steam as is needed at any given time, providing an efficient and responsive approach to variable steam demand.

Modular Design and Reduced Disruption

The modular design provides significant benefits when maintenance is required. Individual systems or modules can be serviced without necessarily interrupting normal operations, helping customers maintain continuity across their wider production processes.

The containerised plant can be delivered as a complete, factory-assembled package, including pipework, electrical wiring, insulation, controls and ventilation. This reduces the amount of work required on site and can help simplify installation and commissioning.

A Complete Steam Solution

By combining ATEX-rated engineering, advanced automation, rapid steam generation and modular construction, the containerised steam system provides a complete solution for challenging industrial environments.

For refineries and other potentially explosive areas, it offers customers greater flexibility over plant location and installation while providing reliable steam generation with minimal operational complexity.

Specialist engineering. Flexible installation. Reliable steam generation.

www.certuss.co.uk


Fertilizing with Precision – How Customized Sensors Ensure Every Granule Hits Its Target

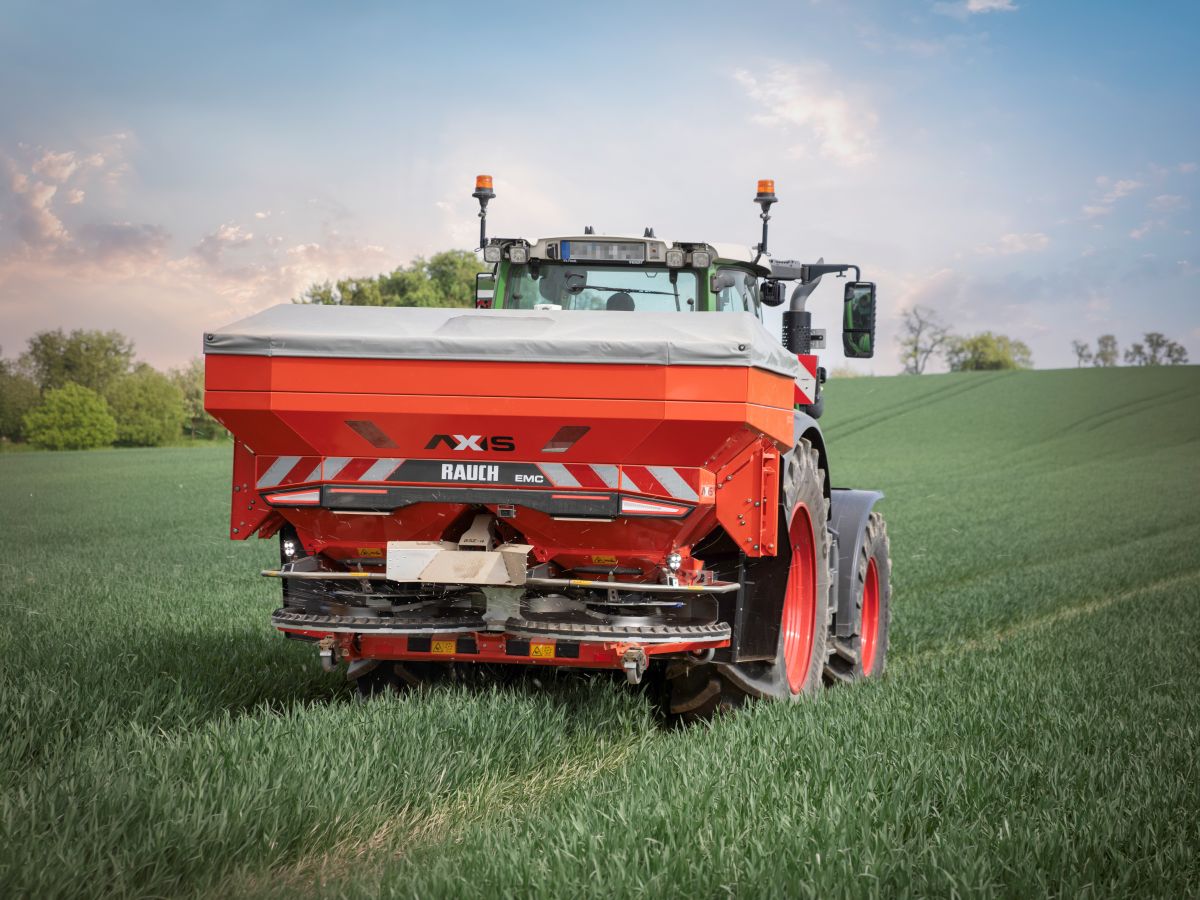
Rauch Landmaschinenfabrik GmbH relies on customized sensors from Metallux AG for its high-precision fertilizer spreaders. They ensure that every application of fertilizer reaches exactly where it is needed – economically, sustainably and with centimeter-level precision.

Rauch Landmaschinenfabrik GmbH is an internationally active family-owned company founded in 1921 and headquartered in Rheinmünster, Germany. The company develops and manufactures high-precision fertilizer spreading and seeding technology for agriculture as well as spreading equipment for winter road maintenance.

Around 400 employees contribute to the company’s success worldwide, including 45 in the development department alone. Its products are distributed in more than 50 countries through an international dealer network.

In the field of fertilizer technology, Rauch uses, among other solutions, disc spreaders in which rotating spreading discs distribute fertilizer granules across the field in precisely calculated trajectories, achieving working widths of up to 54 meters. Precise, targeted distribution depends on the exact coordination of disc speed, drop point and the properties of the fertilizer being used. Depending on particle size, shape and density, each granule has different flight characteristics and is therefore distributed differently across the field.

The objective is clear: to apply the right amount of fertilizer in exactly the right place. For farmers, this is crucial. Fertilizer supplies plants with essential nutrients, helps ensure high yields and contributes to long-term soil fertility. At the same time, it represents a significant cost factor. Under-application can lead to yield losses, while over-application not only causes unnecessary costs but can also impact the environment through excess nutrients entering soil and water. 

Rauch values Metallux for its combination of technical expertise, flexibility and quality. Maximilian Zimmer, Team Leader Product Electronics Development, explains:

“What we value about Metallux is its high level of expertise and reliability. You know what you are getting and can rely on your partner. The geographical proximity was an additional advantage, as it allowed us to discuss matters in person and make decisions quickly. This was particularly important for this project because the technology can only be tested during specific cycles and within limited time windows. Despite the tight schedule, we worked together to develop a very good, customized solution within a short period of time.”

With this solution, fertilizer reaches exactly where it can deliver the greatest benefit. In this way, precision in the field truly bears fruit.

www.metallux.de


British Safety Council’s Annual Conference to address hidden hazards in the workplace

British Safety Council has announced details of its Annual Conference 2026, which this year will examine risks that are often overlooked or underestimated but can have profound consequences for workers' health and wellbeing.

Building on British Safety Council's recently launched Hidden Hazards campaign, the event will focus on practical solutions, policy discussions and real-world examples designed to help organisations identify, manage and prevent long-term occupational health risks.

Called 'Hidden Hazards – From Awareness to Action', the conference will be a free virtual event and take place over two half days on 20 and 21 October. It will bring together health, safety and wellbeing professionals, industry leaders and subject matter experts to explore some of the most significant hidden hazards affecting today's workplaces.

Commenting ahead of the event, Paul Fakley, Marketing and Engagement Director at British Safety Council, who will be chairing the conference, said:

"British Safety Council believes that no one should be injured or made ill through their work. Many of the most serious workplace health risks are not immediately visible, yet they have the potential to cause life-changing harm. Through our Annual Conference this year we aim to bring these hidden hazards into sharper focus and equip organisations with the knowledge, tools and practical solutions needed to protect their people.

"By bringing together leading experts, employers and practitioners at our Annual Conference, we hope to inspire action that creates safer, healthier and more sustainable workplaces for everyone."

The programme includes panel discussions, presentations, case studies and expert sessions on critical workplace issues such as concern around exposure to respirable crystalline silica and the rise of silicosis linked to engineered stone, the realities of indoor and outdoor air quality, the long-term impacts of asbestos exposure, and the increasing importance of addressing workplace stressors, violence and aggression towards employees.

Day one will seek to explore the hidden hazards and raise awareness about them. Day two will focus on policy, leadership and organisational responses required to tackle them effectively. Delegates will hear from experts about the role of technology, leadership and data in driving meaningful change, and learn from organisations that have successfully implemented initiatives to protect worker health and wellbeing.

The conference will feature a keynote address by Prof. Neil Greenberg, President of the Society of Occupational Medicine (SOM), as well as expert contributions from Sarah Sleet, CEO of Asthma and Lung UK, Kevin Bampton, Chief Executive Officer of British Occupational Hygiene Society, Graham Petersen from the Trade Union Clean Air Network (TUCAN), Livi Elsmore, Senior Campaign Manager at the Healthy Air Coalition, Charles Pickles, Founder of Airtight on Asbestos Campaign, John Pares, Chair of the International Institute of Risk and Safety Management (IIRSM), Emily Agyeman, National Federation of Builders and Aurélie Faugier from the Global Cooksafe Coalition, among others.

The event will also include lived experience of living with the consequences of exposure to some hidden hazards, as well as best practise examples of initiatives to tackle and prevent them.

To view the full agenda and register for a free place, visit: https://www.britsafe.org/awards-and-events/conferences/annual-conference-2026